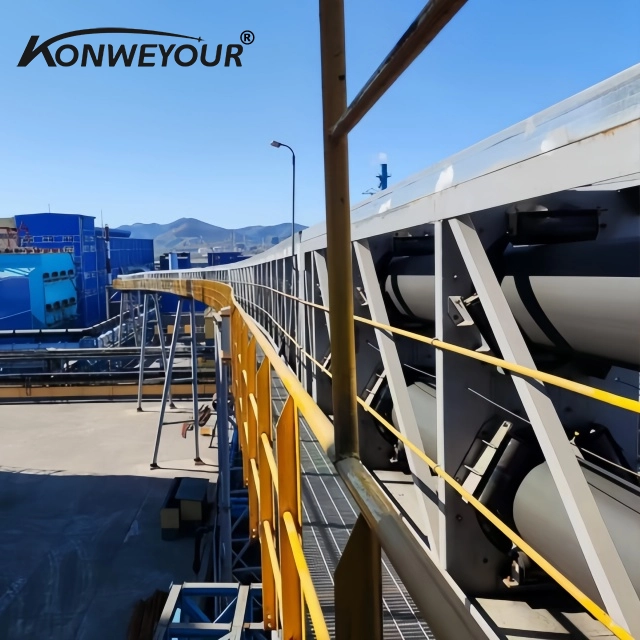
Enclosed Tubular Belt Conveyor
Our Enclosed Tubular Belt Conveyor features a fully enclosed design for clean, efficient, and dust-free bulk material handling over long distances. It is a durable, flexible tubular belt system designed for environmentally sensitive and space-constrained applications, supporting safe transport with minimal spillage and contamination.
Our Enclosed Tubular Belt Conveyor features a fully enclosed design for clean, efficient, and dust-free bulk material handling over long distances. It is a durable, flexible tubular belt system designed for environmentally sensitive and space-constrained applications, supporting safe transport with minimal spillage and contamination.
Enclosed Tubular Belt Conveyor
The Enclosed Tubular Belt Conveyor is an innovative conveying system designed for clean, efficient, and environmentally responsible bulk material transport. Its fully enclosed tubular design helps prevent material spillage, dust emissions, and product contamination, making it ideal for industries that require strict environmental protection and high hygiene standards.
This conveyor system is highly adaptable to complex layouts, including vertical, horizontal, and curved routes. It enables seamless transport across challenging terrain and within confined spaces. During operation, the flexible belt forms a tubular shape, ensuring safe and efficient material flow while minimizing product degradation.
Key Features
Fully Enclosed Design: Prevents dust, spillage, and material loss to support a cleaner working environment.
Versatile Routing: Supports horizontal, vertical, and curved conveying for maximum layout flexibility.
Gentle Material Handling: Suitable for fragile materials, reducing impact and degradation during transport.
Energy Efficient: Optimized for low power consumption while delivering high throughput over long distances.
Durable Construction: Built with high-quality materials to provide long service life and reliable operation.
Applications
Ideal for industries such as mining, cement, agriculture, food processing, power plants, and chemical plants—particularly where environmental protection and safe bulk material handling are critical.
Product Advantages: Enclosed Tubular Belt Conveyor
Fully enclosed design—environmentally friendly and highly efficient
When the conveyor belt is in operation, it forms a tubular structure that effectively prevents material spillage, dust leakage, and environmental pollution, helping meet environmental protection requirements.
Flexible layout—adaptable to complex operating conditions
It enables horizontal, vertical, and multi-angle curved conveying, making it well suited for narrow spaces and complex terrain.
Flexible conveying—protecting materials
The tubular structure reduces impact and material damage during conveying, and is particularly suitable for transporting granular, powdered, or fragile materials.
Energy-saving and high-efficiency performance
An optimized design reduces energy consumption, supports long-distance and high-capacity transport, and enhances overall production efficiency.
Durable structure and easy maintenance
Manufactured using high-strength materials, the system is wear-resistant and corrosion-resistant, offering a long service life and low maintenance costs.
Broad range of applications
Widely used in industries including mining, building materials, cement, power engineering, chemical processing, and grain processing.